Visible Casting Defect Inspection: How the Process Works
Define casting defects, prove camera visibility, connect each result to its casting and challenge further samples before accepting an inspection process.
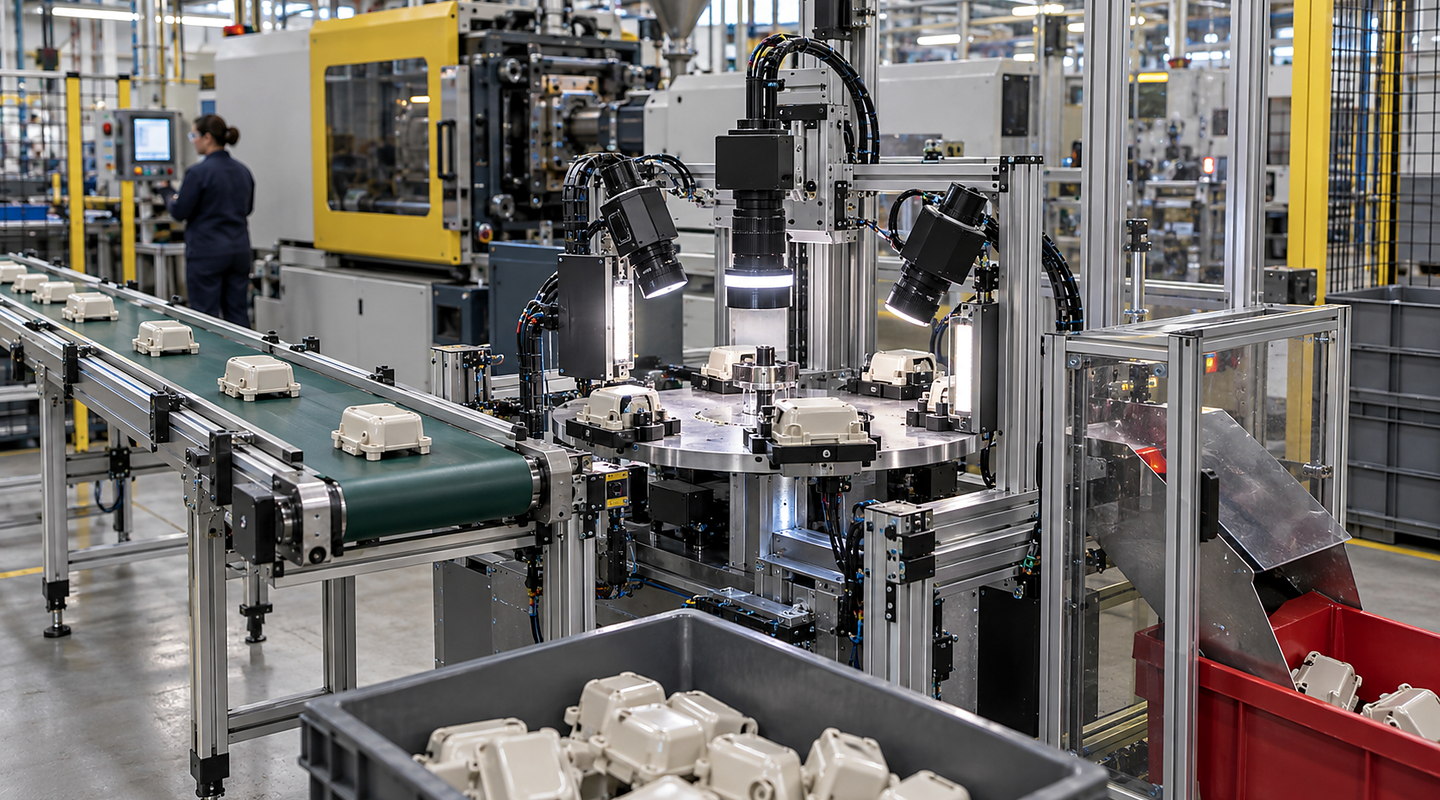
Photographs illustrate general machine-vision inspection. Casting suitability must be assessed using representative castings, defined visible defects and the actual presentation.
Begin with defined visible casting defects and representative samples. Prove that the required regions are observable with the intended presentation and lighting, connect each result to its casting through reject or review, then challenge further samples and document demonstrated coverage.
Use the defect-definition study to establish the acceptance boundary and the challenge-test checklist to record outcomes. Camera visibility must be demonstrated separately from hidden or functional tests.
Understand the complete route from input to accepted output — Visible Casting Defect Inspection
Plan visible casting defect inspection around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems. Follow the material or part through each operating step and include recovery, cleaning and change in the real cycle.
Discuss your application

Four clear stages for visible casting defect inspection
At each stage, you can review how visible defect or measurement definition for visible casting-defect inspection and false-accept, false-reject and challenge criteria affect the next commitment.
- 01
Define the Visible Decision and Collect Representative Samples
Map the inspected faces and label the visible reject conditions. Include normal good parts, defective examples and marginal cases, with surface variation and the approved acceptance boundary.
- 02
Prove Contrast, Presentation and Timing in an Optical Trial
Trial the intended datum, orientation, support, timing and lighting. Compare images of good and defective regions and record recesses, shadows and faces the arrangement cannot assess.
- 03
Integrate Cameras, Controls, Reject Handling and Recipes
Agree the active recipe and part-linked reject, rework or review route. Include missing parts, unexpected variants and interrupted cycles so an inspection result stays with the correct casting.
- 04
Challenge Marginal Cases and Document Agreed Results
Challenge further representative parts after development. Review missed defects and rejected good parts separately, retaining sample identities, conditions, demonstrated coverage and unresolved requirements.
Decisions and results stay connected
| Stage | What happens | What you can review |
|---|---|---|
| Define the Visible Decision and Collect Representative Samples | Map the inspected faces and label the visible reject conditions. Include normal good parts, defective examples and marginal cases, with surface variation and the approved acceptance boundary. | Drawing regions, labelled sample identities, acceptable surface variation and the approved decision boundary. |
| Prove Contrast, Presentation and Timing in an Optical Trial | Trial the intended datum, orientation, support, timing and lighting. Compare images of good and defective regions and record recesses, shadows and faces the arrangement cannot assess. | Camera views, part presentation, timing and lighting, with excluded regions and uncertain visibility recorded. |
| Integrate Cameras, Controls, Reject Handling and Recipes | Agree the active recipe and part-linked reject, rework or review route. Include missing parts, unexpected variants and interrupted cycles so an inspection result stays with the correct casting. | Recipe and interface record, casting-to-result tracking and the observed reject, rework or review outcome. |
| Challenge Marginal Cases and Document Agreed Results | Challenge further representative parts after development. Review missed defects and rejected good parts separately, retaining sample identities, conditions, demonstrated coverage and unresolved requirements. | Further sample results, separate missed-defect and rejected-good counts, demonstrated coverage and open requirements. |
Keep connected responsibilities clear
Your final visible casting defect inspection scope must also account for recipe, reject and line-control interfaces, false-accept, false-reject and challenge criteria, current regulations and the conditions at your site.
- A camera can only assess a property made visible and repeatable by the inspection setup.
- Sample diversity and marginal cases determine how meaningful a feasibility result is.
- Visual inspection does not replace hidden, destructive, functional or statutory tests.